TA2 commercially pure titanium · HF(5%)+HNO₃(30%)
Chemical Etching Formula
TA2 commercially pure titanium
with HF(5%)+HNO₃(30%)
Formula Summary
The table below summarizes every parameter that defines this etching formula. Values listed as ranges scale with sheet thickness across the supported band.
Why HF(5%)+HNO₃(30%) for TA2 commercially pure titanium?
For TA2 commercially pure titanium, the HF/HNO₃ blend works where chloride chemistries stall: fluoride dissolves the stable oxide, nitric acid re-oxidizes the metal, and the two cycle to give a steady etch. Concentration and temperature control are critical here because the rate is strongly chemistry-dependent.
Process Window & Bath Control
Hold the bath at 33°C with concentration as specified (specific gravity 1.180). Across the 0.05-0.5 mm thickness range, conveyor speed runs from 0.12-1.36 m/min — thinner sheets move faster, thicker sheets slower, in roughly inverse proportion to thickness. A typical mid-range setpoint is 0.17 m/min for 0.18 mm stock. Use redundant PID temperature control to hold the bath within ±1.5°C, and titrate at least once per shift.
Design Rules & Tolerances
Feature sizes scale with sheet thickness. For this formula the minimum hole diameter ranges 60-600 μm and the minimum line width ranges 100-500 μm across the 0.05-0.5 mm band, following the industry 1.2× (hole) and 1.0× (line) thickness rules. Single-side undercut ranges 11-107 μm, and the etch factor is about 2.33. Size your photomask by subtracting twice the expected undercut from each finished feature dimension.
• Minimum hole diameter range: 60-600 μm
• Minimum line width range: 100-500 μm
• Single-side undercut range: 11-107 μm
• Typical etch factor (EF): 2.33
Yield & Production Economics
Typical mass-production yield for TA2 commercially pure titanium in the HF(5%)+HNO₃(30%) system is 95.1%, within an observed range of 94.2-95.4%. The dominant yield-loss modes are photoresist pinhole defects and rinse-water contamination. Improving incoming sheet quality and photoresist coating consistency gives the highest yield-improvement leverage for this formula.
Typical Applications
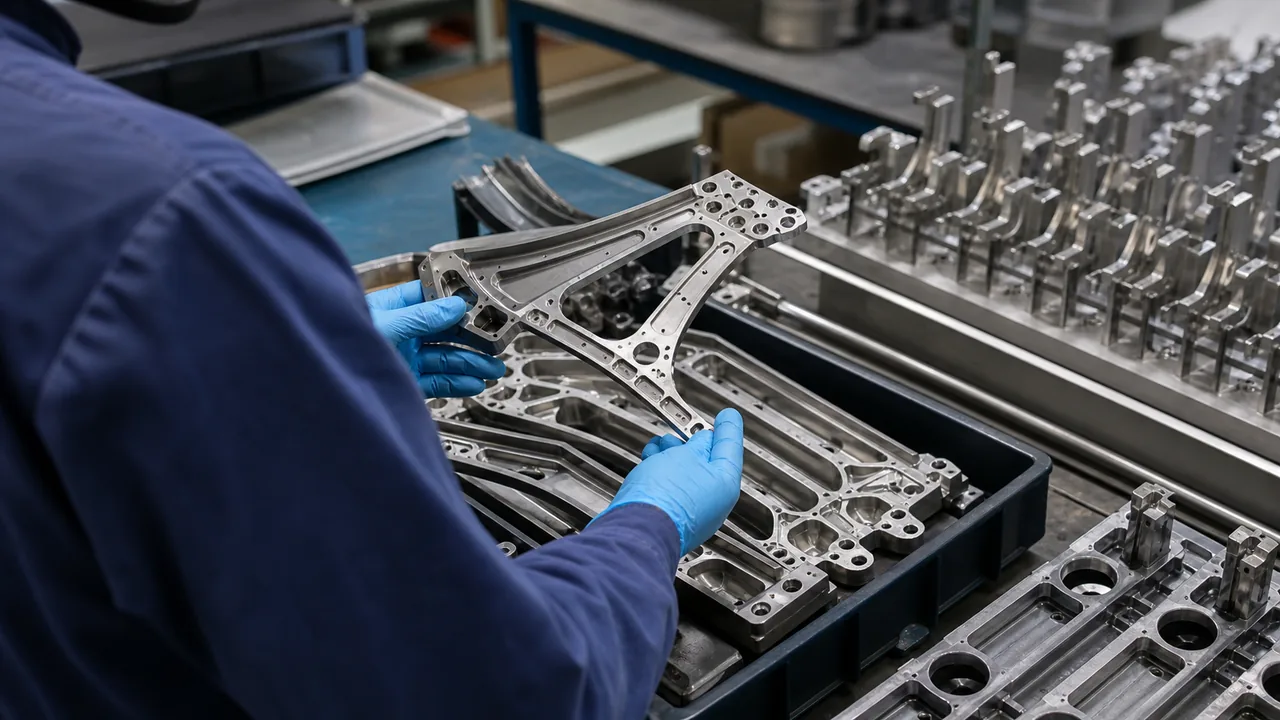
TA2 commercially pure titanium etched with this recipe typically ends up in medical implants, surgical instruments, aerospace brackets, and corrosion-resistant filters. Because chemical etching applies no mechanical or thermal load, the finished features are free of work-hardening and heat-affected zones — a decisive advantage over stamping or laser cutting for these uses.
Process Equipment & Material Reference
Production of TA2 commercially pure titanium parts using the HF(5%)+HNO₃(30%) formula described above runs on a knife-mold etching machine configured for through etch (double-sided). The bath chemistry, conveyor speed, and rinse cascade detailed on this page reflect the operating profile we use on a live spray-etching line for this alloy.
Related to this formula, the Titanium chemical etching guide page documents the full process envelope for the same alloy family, including pre-treatment chemistry and post-etch inspection criteria.
Production Use Cases for This Formula
Typical end-uses for TA2 commercially pure titanium run on this formula include high-speed air-intake mesh for hair dryers, stainless steel mesh for aroma diffusers, and cold-press juicer filtration mesh. The 33°C bath and 0.05-0.5 mm supported thickness range cover most of the production work in these segments without re-tuning chemistry.
Adjacent applications usually transfer onto this same formula with no chemistry change, sometimes only a conveyor speed tweak. Drop a drawing and a target volume and we will return a process card built off the parameters on this page.
More Titanium Alloys Formulas
Other formulas in the same material family.
Frequently Asked Questions
Sources & References
- ASTM E407: Standard Practice for Microetching Metals and Alloys
- ASTM B912: Standard Specification for Passivation of Stainless Steels
- Photo Chemical Machining Institute — process capability guidelines
- NIST Engineering Statistics Handbook — process tolerance and capability
Standards are referenced for context. Always confirm parameters against the current published edition and your own process validation.
Need a Quote for This Process?
WET Etched runs production wet chemical etching lines using the HF(5%)+HNO₃(30%) chemistry. Send us your part drawing and quantity for a full process quote.